If you’ve ever worked with HDPE pipe machinery, you know that a well-fitted die is the difference between uniform, durable pipe that meets industry standards and messy, inconsistent output that wastes material and time. As a supplier of HDPE pipe machines, I’ve spent over a decade walking new operators through this process—many of whom come to us straight out of trade school, or have been struggling with frequent die changes that leave their production lines down for hours. Today, I’m pulling back the curtain on exactly how to install an HDPE pipe machine die, step by step, with the small, real-world tips I’ve learned that don’t make it into generic operation manuals. No fluff, no confusing jargon, just what actually works when you’re standing in front of your machine at 7 a.m. ready to start a production run. HDPE Pipe Machine
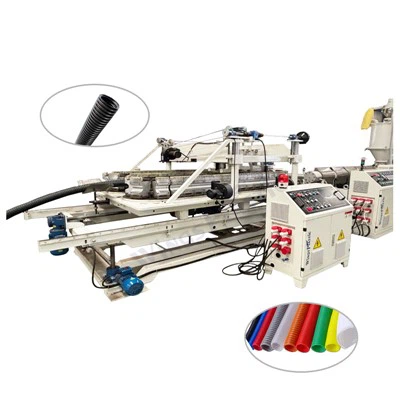
First, let’s get one critical thing out of the way: safety. I can’t stress this enough, especially for anyone new to these machines. HDPE pipe dies operate at extreme temperatures—often between 180°C and 230°C, depending on the grade of HDPE you’re using—so even a small touch to a component can cause a severe burn. Always disconnect the machine from its power source before touching any die parts, and let the barrel cool slightly if you’ve just finished a run with high-temperature resin. Wear heat-resistant gloves, safety glasses, and closed-toe work boots. I learned this the hard way early in my career, when a loose heat shield slipped and I burned my wrist so badly I was out for a week. Don’t be that guy.
Before you even grab a wrench, you need to prep the work area and gather the right tools. Rushing this step is where most mistakes happen, and it’s the number one reason our service team gets called out for “bad die fits” that were actually avoidable. You’ll need a set of metric wrenches (most HDPE pipe machine dies use 12mm, 14mm, and 17mm bolts), a torque wrench set to the manufacturer’s specified torque for your die (this varies by machine model, so keep that manual handy), a soft-bristle brush, isopropyl alcohol or a specialized plastic cleaning solvent (avoid acetone—it can leave a residue that ruins HDPE flow), and a clean lint-free cloth. Also, clear a 3-foot area around the machine so you have space to lay out the die components without knocking anything over. I keep a small parts tray marked “die hardware” next to every work area, because losing a single lock washer can add an extra hour to your install.
Next, remove the old die. If you’re replacing a die because it’s worn out or you’re switching pipe diameters, first turn off the extruder and let it cool for at least 30 minutes. Never try to remove a hot die—you’ll risk damaging the alignment pins on the machine barrel, which are the key to uniform pipe wall thickness. Once cooled, locate the four to six hex bolts holding the die to the machine’s adapter plate. Loosen them in a crisscross pattern, not just one bolt all the way first. This distributes pressure evenly and prevents the adapter plate from warping, which is a common issue I see with operators who skip this step. As you loosen the bolts, hold the die firmly—they’re heavy, often 20 to 50 pounds depending on the pipe size, and can slip if you’re not paying attention. Once all bolts are loose, wiggle the die gently to separate it from the adapter plate, and set it on your parts tray. Don’t set it directly on the floor—debris or metal shavings can get into the die’s lip, which will cause ripples in your new pipe.
Now, the most important step for a long-lasting die fit: cleaning the mating surfaces. The adapter plate and the back of the old die will have a thin layer of residual HDPE, carbon buildup, and dust from the plant floor. If you don’t remove this, the new die won’t sit flush, which will lead to uneven extrusion, leaks, and even die damage over time. Use your soft brush to gently sweep away loose debris, then dampen a lint-free cloth with isopropyl alcohol and wipe both surfaces thoroughly. For tough, baked-on HDPE buildup, a plastic scraper works—never use a metal one, as it can scratch the mating surface and create tiny gaps that will ruin pipe quality. I always do a second wipe with a fresh cloth to make sure no residue is left, because even a tiny fleck of old HDPE is enough to cause a thin spot in a 12-inch pipe.
Once the mating surfaces are clean, it’s time to align the new die. This is where the alignment pins come into play—every HDPE pipe machine has two precision pins on the adapter plate that fit into matching holes on the back of the die. These pins ensure the die’s internal flow channels line up perfectly with the extruder barrel, which is non-negotiable for uniform pipe wall thickness. Pick up your new die, line up the pin holes with the adapter plate’s pins, and push it straight on—don’t twist it as you seat it. If it doesn’t slide on easily, double-check that the pins aren’t bent (sometimes they get knocked out of alignment during die changes) and that there’s no debris left on the mating surface. I once had an operator tell me his die wouldn’t seat, and we found a small piece of plastic chip wedged under one pin that he’d missed when cleaning. It took 10 seconds to remove, and he’d wasted 20 minutes struggling.
With the die seated on the pins, it’s time to install the and tighten the bolts. First, thread all the bolts by hand to make sure they start straight—cross-threaded bolts are a quick way to ruin a die or adapter plate. Once all bolts are finger-tight, use your wrench to tighten them in that same crisscross pattern. Start with the top-left bolt, then the bottom-right, then top-right, then bottom-left, and repeat this cycle until each bolt is about halfway tight. Don’t use a torque wrench yet—this initial step is to seat the die evenly. Once all bolts are snug, switch to your torque wrench and tighten them to the exact specification listed in your machine manual. For most mid-sized HDPE pipe machines, that’s between 15 and 20 Nm, but always confirm for your model. Over-tightening is just as bad as under-tightening; it can warp the die’s housing, bend the pins, or cause the bolt to snap off mid-run. I’ve seen a new operator over-tighten bolts on a 16-inch die, and the die cracked before they even ran a foot of pipe.
After tightening the bolts, a final check is critical. Gently tug on the die to make sure it doesn’t move at all—if it wiggles, your bolts are uneven, and you’ll get inconsistent pipe. Next, inspect the die’s lip (the part that forms the outside of the pipe) for any damage or debris. Even a tiny burr on the lip can cause a jagged edge on the pipe, which will fail pressure tests. If you notice any issues, stop and fix them before starting the machine. Also, double-check that all heat bands (if your die has them) are connected properly—loose wires here can cause uneven heating, leading to melted HDPE drips or lumpy pipe.
Now that the die is installed, you’re ready to run a test run. Turn on the extruder and set the temperature to your resin’s recommended level, then let the die heat for 30 to 45 minutes before pushing any HDPE. This gives the die time to reach uniform temperature, which is essential for consistent extrusion. Once heated, run a small amount of scrap HDPE through the extruder to purge any air left in the lines, then start pulling a test piece of pipe. Check for uniform wall thickness, smooth outer and inner surfaces, and no ripples or leaks. If everything looks good, you’re ready to start your production run. If you notice issues like thin spots or uneven flow, turn off the machine immediately and check your die alignment or torque settings—most of the time, it’s a small fix.
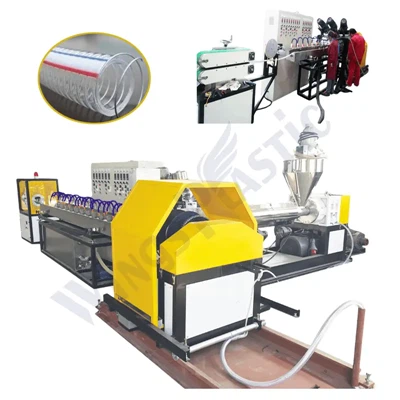
As someone who supplies HDPE pipe machines and supports hundreds of operators across North America and Europe, I know that proper die installation isn’t just a step in a manual—it’s the foundation of efficient, high-quality production. Skipping steps like cleaning mating surfaces or using the wrong torque wastes time, materials, and money. A well-installed die can last for years, while a poorly fitted one will need replacement in months. If you’re new to working with HDPE pipe machines, don’t be afraid to ask questions—our team offers free training for all the machines we sell, and we’re always here to help when you run into issues. If you’re looking to upgrade your HDPE pipe machine fleet or need support with die installation, reach out to our sales team to discuss your specific needs. We work with small fabricators and large pipeline contractors alike, and we’re committed to helping you run your operation as smoothly as possible.
PVC Pipe Machine References:
- Plastics Pipe Institute. (2020). HDPE Pipe Extrusion: Die Design and Installation Best Practices. Technical Report TR-4.
- Batson, G. (2017). Extrusion: The Definitive Processing Guide and Handbook (2nd ed.). William Andrew Publishing.
- American Society of Mechanical Engineers. (2019). Standard for Safety of Plastic Extrusion Machinery. ASME B151.1.
Qingdao Wings Plastic Technology Co., Ltd.
As one of the most experienced hdpe pipe machine manufacturers and suppliers in China, we also support customized service. Please feel free to buy durable hdpe pipe machine made in China here from our factory. For price consultation, contact us.
Address: C02 Of Anshengyi Road, No.2 Fuan Industry Zone,Jiaodong Town, Jiaozhou City, Qingdao City, Shandong Province,China
E-mail: kelly@wingsplastic.com
WebSite: https://www.wingsextruder.com/
